
Views: 0 Author: Site Editor Publish Time: 2026-09-12 Origin: Site


Are high defect rates eating into your factory margins? Flawless sanitaryware demands more than premium clay. It requires absolute precision on the factory floor. Poor calibration wastes raw materials rapidly. It bottlenecks your entire production line and frustrates your engineering team.
In this comprehensive guide, we walk through the essential setup checks required before initiating a production cycle. We cover everything from microscopic tooling alignment to hydraulic pressure calibration. By strictly following these protocols, you ensure your High Pressure Casting Machine runs perfectly from the very first cycle. This proactive approach safeguards your bottom-line profitability and extends equipment lifespan.
Before putting a wrench to any bolt, operators must understand the fundamental mechanics of the equipment in front of them. This machinery represents a significant capital investment. It is explicitly designed to replace traditional, labor-intensive plaster casting with automated, physics-driven precision.
The entire process relies heavily on fluid dynamics and material science. Unlike traditional methods that depend on the slow capillary action of dry plaster, this technology forces liquid ceramic slip into a porous polymer cavity under elevated pressure. This pressure typically hovers between 10 to 15 bar. When the pressurized slip fills the void, the water content is violently pushed through a microscopic capillary network. This rapid dewatering process leaves solid clay particles packed tightly against the wall. Consequently, it forms the basin body in a fraction of the time required by atmospheric casting.
Recent industry analyses reveal a massive shift in sanitaryware manufacturing. Driven by strict environmental regulations regarding industrial water waste and soaring global energy costs, major facilities are abandoning traditional plaster casting. Instead, they are rapidly adopting automated high-pressure systems. This transition is not merely about speed. It is about survival in a highly competitive market that demands sustainable, zero-waste production. Modern automated casting technologies drastically reduce water consumption and minimize scrap rates.
However, this technological leap means operator expertise must also evolve. A miscalibrated automated system can produce defects at a terrifying speed. Empirical data from top-tier factories indicates that setup precision directly correlates with overall profitability. A meticulously calibrated setup drops a standard six-hour plaster casting process down to a mere 15 to 25 minutes. Furthermore, it prevents slip leakage and protects your expensive tooling from premature failure.
Think of the polymer cavity as the heart of your operation. It is the most critical interface between the mechanical beast and the delicate final product. Any oversight during its installation mathematically guarantees structural flaws in your wash basins.
A multi-part Resin Mould must be aligned with micrometer precision. Before hoisting the blocks into the press, floor technicians should wipe down the steel platens with a microfiber cloth. Stray clay particles easily throw off the seating. Using dial indicators, engineers must verify that the male and female components mate perfectly. Even a half-millimeter misalignment results in severe flashing. Flashing is a stubborn defect where excess clay seeps into the seam lines, requiring expensive manual trimming later.
To counteract asymmetrical stress, operators must follow a strict cross-pattern tightening sequence for all fastening bolts. Utilizing a calibrated torque wrench ensures every bolt meets the manufacturer specified torque. This prevents the tooling from warping under intense clamping pressure.
The efficiency of the dewatering process relies entirely on the uniform porosity of the cavity surface. Before closing the machine, conduct a thorough visual and tactile inspection under bright, angled lighting. Look for micro-cracks around complex geometric areas like the drain hole or overflow channel. These pinch-points experience the highest fluid velocity. In addition, run a gloved hand over the surface to check for localized blinding. Blinding refers to pore blockages caused by fine clay particles embedded in the matrix. A blocked area will refuse to absorb water, leaving a dangerously thin and mushy spot in the basin wall.
Old slip residue left inside the internal pipe network is a silent killer of casting cycles. Before the very first run of the shift, the capillary network must be systematically purged. Run a sequence of high-pressure water and compressed air through the internal channels. Listen for the distinct hiss of air clearing the lines. Visually verify that the water exiting the purge valves runs completely clear. If the discharge appears milky, repeat the flushing cycle until the internal network is pristine.
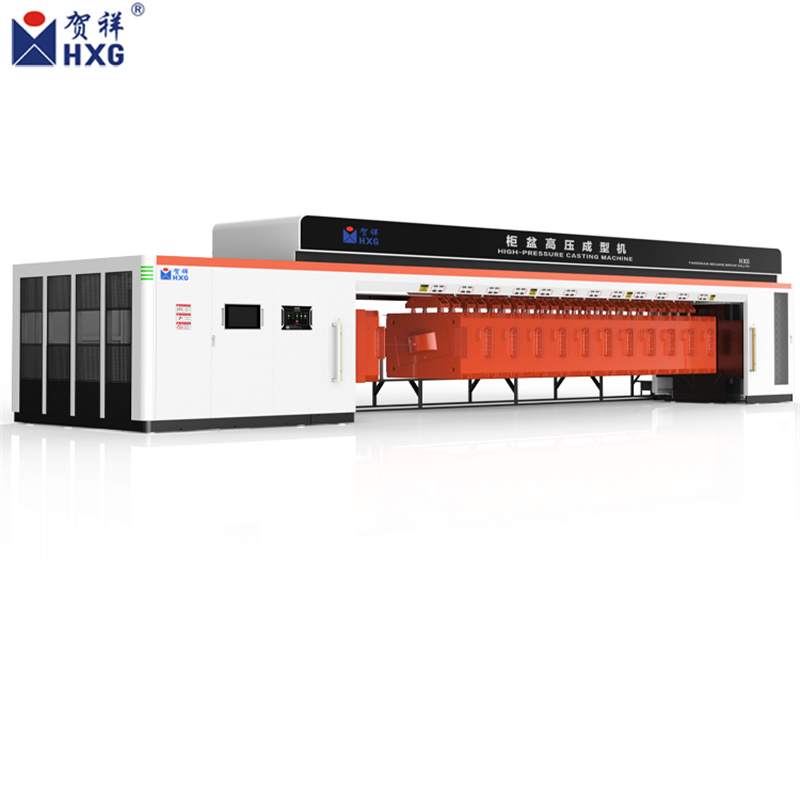
The physical muscle of the Wash Basin HPCM is generated by its hydraulic power unit. It must provide enough brute force to keep the heavy platens locked against the intense internal pressure of the injected slip. Yet, it must deliver this force with controlled and stable precision.
Because hydraulic systems operate on the principle of fluid incompressibility, the oil must be in optimal condition. Check the reservoir sight glass to ensure the fluid sits comfortably in the upper half of the gauge. Equally important is the thermal state of the oil. Hydraulic fluid changes viscosity based on temperature. If the oil is cold, cylinder movements become sluggish, throwing off the delicate timing of your casting recipe. Conversely, if it exceeds 55 degrees Celsius, the fluid degrades and seals begin to harden. Ensure the integrated water-cooling heat exchanger is functioning to keep the oil in the sweet spot of 40 to 50 degrees Celsius.
Dialing in the clamping pressure is an exercise in applied physics. The holding force must exceed the internal separating force generated by the pressurized slip. The math is straightforward. You multiply the injection pressure by the projected area of the basin cavity. For instance, if the slip hits 12 bar and the basin features a wide profile, the separating force is immense. The hydraulic cylinders must be programmed to deliver a tonnage typically up to 400 kN, including a 20 percent safety margin above the calculated force. Setting it too low guarantees a violent and hazardous slip blowout from the seams. Setting it unnecessarily high applies crushing stress that eventually collapses the internal porous structure of your tooling.
A pressurized system under heavy load quickly exposes plumbing weaknesses. Walk the perimeter of the machine with a flashlight. Inspect all high-pressure hoses, manifold fittings, and cylinder rod seals. Look for weeping oil or accumulated grime that indicates a slow leak. Even a minor drop in line pressure reduces the system ability to maintain a rigid hold during the casting cycle. This leads to micro-fluctuations that can fracture the wash basin before the press even opens.
To bridge the gap between theory and factory floor execution, we rely on strict parameter control. Below is a quick-reference matrix highlighting critical setup ranges and the direct consequences of miscalibration.
Setup Parameter | Optimal Range | Defect if Miscalibrated |
|---|---|---|
Slip Specific Gravity | 1.80 to 1.85 g/cm³ | Soft green body or extended cycle times |
Slip Temperature | 30 to 35 Degrees Celsius | Poor fluidity causing uneven wall thickness |
Demoulding Air Pressure | 1.5 to 2.0 Bar | Basin tearing or sticking to the cavity |
Water Flush Pressure | 3.0 to 5.0 Bar | Irreversible pore calcification and blinding |
The most sophisticated automated press cannot compensate for poorly prepared raw materials. Ceramic slip is a non-Newtonian fluid. Its flow behavior shifts dramatically under pressure. Preparing it correctly remains a strict scientific prerequisite.
Before the liquid clay is pumped into the pressure tanks, it must pass rigorous laboratory testing. The specific gravity determines the solid-to-water ratio. If the density drops below target levels, the machine wastes valuable cycle time squeezing out excess water. This results in a soft and unstable green body.
Viscosity is equally critical. Using a torsion viscometer, technicians measure the slip thixotropy. This is its ability to flow when agitated and thicken when at rest. The mixture must be fluid enough to navigate the intricate corners of the wash basin geometry under pressure. Simultaneously, it must be thick enough to suspend heavy silica and feldspar particles without them settling out at the bottom of the tank.
Thermodynamics play a hidden but vital role on the factory floor. The temperature of the slip directly affects its viscosity and the capillary draw of the polymer pores. Maintaining the slip between 30 and 35 degrees Celsius yields the most consistent casting rates. Cold slip thickens up, requiring higher injection pressures that unnecessarily stress the equipment. Utilize temperature-controlled storage tanks with slow-moving agitators to maintain a homogeneous thermal state.
The delivery mechanism must be calibrated to match the exact pressure curve programmed into the control system. High-pressure casting is not a single-pressure event. It begins with a gentle low-pressure fill to evacuate air from the cavity without causing turbulence. Once full, the system ramps up to the high-pressure holding phase to consolidate the clay wall. Verify that your diaphragm pumps or pressurized tanks hit these targets seamlessly. Cross-reference your digital transducers against analog master gauges to confirm accuracy.
The final phase of the casting cycle is often the most delicate. Extracting the newly formed and fragile wash basin relies on a highly synchronized interplay of compressed air and filtered water.
Immediately after the excess slip is drained from the core, the system must clean the tooling. High-pressure water is injected into the internal network to back-flush the pores. Set this water pressure carefully, usually between 3 to 5 bar. It must be strong enough to overcome capillary resistance and push residual clay out. However, it must be gentle enough not to rupture the internal piping. Always ensure this water is highly filtered. Introducing hard water or particulate-laden fluid permanently calcifies the micro-pores.
Once flushed, compressed air is introduced to push the remaining water to the surface. This creates a microscopic film of moisture between the cavity wall and the clay basin, acting as a frictionless release agent. If the demoulding air pressure is too aggressive, it blows a hole straight through the soft clay. If it is too weak, the basin sticks and tears. Calibrate the regulators to provide a gentle and sustained pressure around 1.5 to 2 bar. This slowly releases the vacuum hold, allowing the automated handling robot to extract the piece safely.
The Programmable Logic Controller acts as the brain of the operation. Feeding it the correct parameters transforms raw mechanical power into a refined manufacturing process.
Different wash basin designs require vastly different control recipes. A thin-walled countertop vessel behaves differently than a thick pedestal sink. The operator must select the correct program that dictates slip injection time, high-pressure holding duration, and the precise timing of the decompression curve. Venting the internal pressure too rapidly causes trapped moisture in the clay to expand violently, fracturing the basin instantly.
Before switching to fully automatic mode on your Basin Casting Machine, physically test all proximity sensors and limit switches. These electronic eyes tell the main computer that the platens are fully closed and locked. Wave a metal test wand over the inductive sensors to ensure the control panel registers the input instantly. This simple check prevents the machine from injecting high-pressure slip into a partially open press.
Validating safety mechanisms is a non-negotiable step. Ensuring these systems are hyper-responsive protects both your floor operators and the structural integrity of the equipment itself.
The emergency stop circuit is your primary failsafe. Physically smash the emergency stop button during a dry run. Verify that it immediately halts all hydraulic pump activity and vents accumulated pneumatic pressure. The system must freeze platen movement within milliseconds. Furthermore, the control system should lock out any automated restart until a supervisor manually clears the fault on the screen.
Optical light curtains must be tested by intentionally breaking the infrared plane with a test rod while the press is closing. The machine must halt or reverse its stroke instantly. In addition, verify that physical safety gates are interlocked with the main injection valve. If a gate is cracked open, the system must physically prevent high-pressure ceramic slip from entering the hazard zone.
Even with precise initial calibration, the complex interaction between fluid dynamics and mechanical clamping often produces unexpected results during the first few test cycles. A systematic approach is required to iron out the kinks.
If you encounter slip leaking from the seams, first verify the hydraulic clamping tonnage via the control panel. If the force is correct, the issue likely stems from micro-misalignment of the blocks. Apply a pressure-sensitive layout fluid to the faces, perform a dry closure, and adjust the platen leveling nuts until the contact pattern is perfectly uniform.
When the green body sticks to the cavity upon opening, it indicates a demoulding failure. Inspect the compressed air regulators to ensure the release pressure peaks at the exact moment the halves separate. If the air supply is fine, initiate a high-pressure water back-flush to clear out occluded resin pores.
If you spot cracks in the unfired basin, your decompression curve is likely too aggressive. Adjust the recipe to implement a stepped and linear pressure release. Also, double-check your slip viscosity. Overly thick slip creates internal stress gradients during injection that manifest as cracks once the physical support of the press is removed.
Setting up the equipment is never a set-and-forget endeavor. Once the initial parameters yield a defect-free wash basin, lock those parameters in the system and establish a baseline for preventative maintenance.
Record the baseline pressure curves, hydraulic temperatures, and exact cycle times. By monitoring these variables week over week, maintenance teams can predict component wear before it causes a breakdown. For example, if the hydraulic pump slowly requires more time to achieve the target clamping tonnage, it is a clear empirical indicator of internal pump wear or fluid bypass in the main cylinder. Daily checks of air dryers and water traps on the pneumatic lines also prevent moisture from corrupting the delicate demoulding sequence.
Proper setup ensures high-quality ceramic wash basins and a streamlined production floor. By meticulously checking your tooling alignment, hydraulic integrity, slip parameters, and control systems, you prevent costly material waste. Always verify your clamping pressures and safety interlocks before initiating a run. While these comprehensive setup checks require patience and precision upfront, they ultimately save thousands of dollars in scrapped products and machine downtime.
Ready to upgrade your sanitaryware production line with industry-leading automation? Ensure your factory stays ahead of the curve by investing in reliable, high-precision equipment. Explore the full range of advanced casting solutions and find the perfect fit for your production needs at HXG Machine today.
The setup duration depends largely on the automation level of the facility and the complexity of the basin geometry. A complete physical changeover of the multi-part tooling requires roughly two to four hours for an experienced engineering team. Following the mechanical setup, recalibrating the control system, testing the slip, and running initial dry cycles adds an additional one to two hours. Allocate a full shift to transition safely and accurately.
Under optimal operating conditions, high-quality porous tooling withstands between 30,000 and 50,000 casting cycles. However, this lifespan is strictly contingent upon meticulous setup and maintenance. Applying excessive clamping force or failing to calibrate the water flushing pressure correctly leads to irreversible micro-fractures and pore clogging. Routine chemical cleaning is required to achieve this maximum lifespan.
Uneven wall thickness is an empirical indicator of fluid dynamic imbalances during the injection phase. This is rarely a mechanical fault, but rather a setup calibration error. The most common cause is an incorrect slip feed pressure. If the slip is injected too slowly, it begins to form a solid layer unevenly before the cavity is fully pressurized. Other culprits include a misaligned core or temperature fluctuations affecting slip viscosity.
Hydraulic fluid integrity is the lifeblood of high-pressure machinery. Visual inspections of the fluid level and temperature gauges should be conducted daily before the first production cycle begins. A more rigorous empirical analysis testing for oil degradation, oxidation, and particulate contamination should be scheduled monthly. This ensures microscopic debris is not scoring the internal walls of your clamping cylinders.
For optimal flow and consistent casting rates, ceramic slip should be maintained between 30 and 35 degrees Celsius. If the temperature drops below 20 degrees Celsius, the slip becomes highly viscous. This requires excessive injection pressure, which strains the pumps and artificially extends the cycle time. Utilizing temperature-controlled, agitated storage tanks is the best way to maintain this thermal sweet spot.
Preventing pore blinding requires strict adherence to the demoulding flush protocols. You must back-flush the cavity with highly filtered water at 3 to 5 bar immediately after every cycle. This pushes residual clay particles out of the micro-capillary network before they can dry and harden. Additionally, scheduling a dedicated chemical flush using specialized mild acids every few weeks dissolves any deep-seated mineral calcification.


